EDM and Wire EDM Services
At SelenPreci, our sinker EDM and wire EDM equipment deliver high-precision machining for intricate custom parts made from hard conductive materials.
As a one-stop CNC manufacturer based in Shenzhen, we handle ultra-complex geometries that traditional CNC milling or turning struggles to produce, for prototypes, small batches and mass production.
Our EDM Capabilities
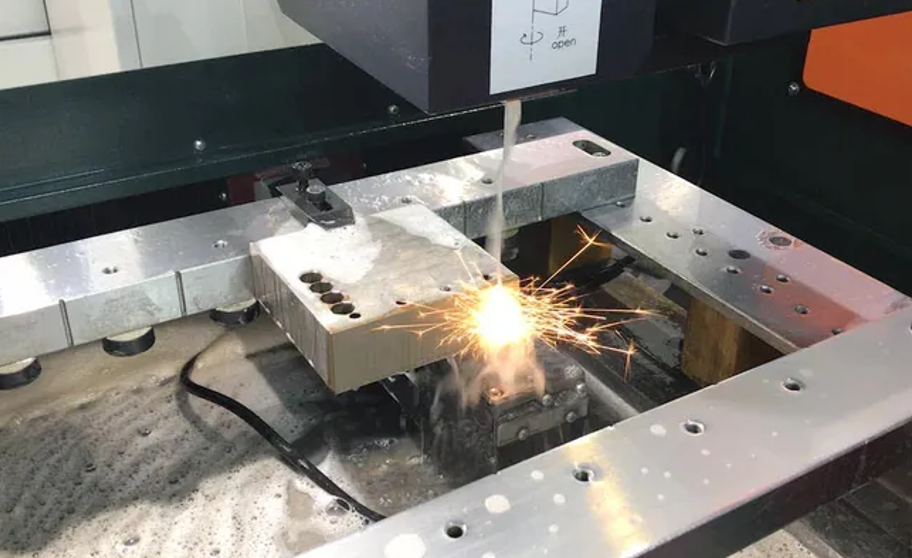
We offer two core electrical discharge machining technologies to manufacture intricate custom components, solving tough machining challenges for hard metals.
Sinker EDM (EDM)
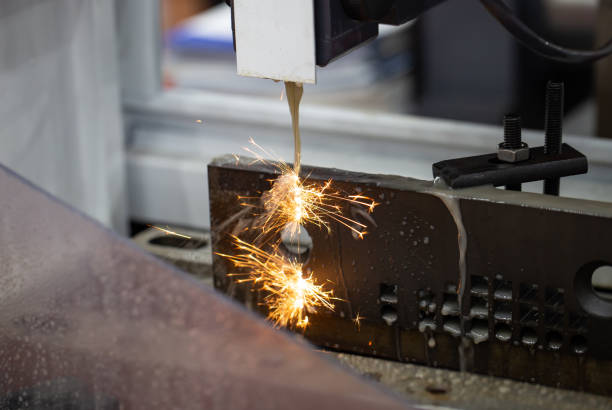
Sinker EDM, also known as cavity EDM, uses controlled electrical sparks to erode workpieces. It excels in creating deep cavities, sharp internal corners, thin walls and fine grooves on hard conductive materials. It is widely used for mold inserts and complex 3D precision parts where conventional cutting tools cannot reach.
Wire EDM (WEDM)
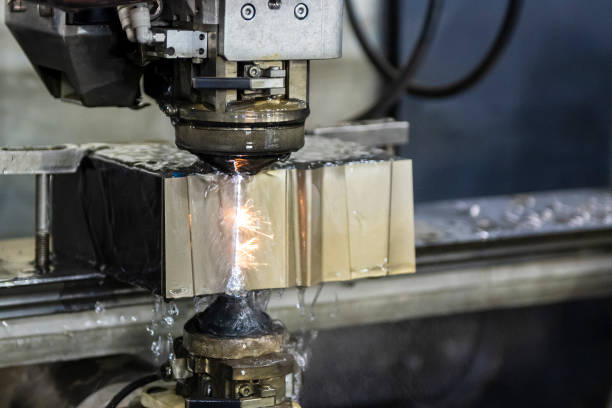
Wire EDM uses a thin travelling metal wire to cut workpieces via electrical discharge. It efficiently fabricates narrow slits, elongated holes, external contours and intricate 2D profiles. This process is ideal for thin, hardened workpieces requiring tight dimensional tolerance and clean cutting edges.
Advantages of EDM and Wire EDM
Electrical discharge machining is a non-contact subtractive manufacturing method for high-precision complex parts. Our in-house EDM services bring great value to your custom manufacturing projects.
Exceptional Precision and Accuracy
EDM and Wire EDM achieve micron-level tight tolerances for intricate geometries. Spark erosion delivers reliable accuracy for ultra-fine features that standard CNC machining cannot reach.
Machining Hard Conductive Materials
This technology works perfectly for hardened tool steel, titanium, carbide and hard alloys. It removes material without cutting force, no matter how hard the conductive workpiece is.
Complex Geometries & Intricate Features
Both processes are perfect for sharp corners, deep cavities, undercuts, micro holes and narrow slots. Sinker EDM handles complex 3D cavities while Wire EDM excels in sharp 2D contours.
Zero Mechanical Stress on Workpieces
No physical cutting force touches the part during spark erosion. It eliminates deformation and warping risks, making it ideal for ultra-thin wall and delicate fragile components.
Controlled Minimal Heat-Affected Zone
We precisely control discharge energy to limit the heat-affected zone. It prevents thermal damage and preserves material performance for heat-sensitive precision parts.
Wide Flexibility for Prototyping & Batch Orders
Our EDM solutions adapt to simple and highly complex custom parts. Flexible for prototype validation, small batch trial runs and volume production to match your project timeline.
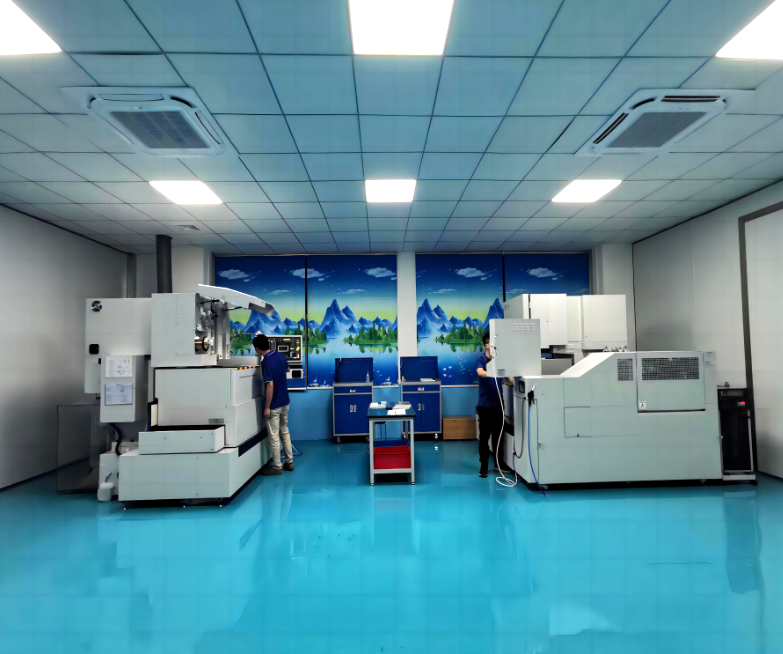
Wire EDM Machining in Our Workshop
Wire EDM is a precision machining process that uses electrical discharges to cut conductive materials along programmed paths. It is particularly suitable for producing intricate profiles, narrow slots, and complex contours that are difficult to achieve with conventional cutting methods.
At SelenPreci, our Wire EDM machining capability supports custom precision components with complex geometries and demanding dimensional requirements. Our workshop is equipped to support different project needs, from prototype development to custom part production.
Typical Applications:
▪ Complex profiles and intricate contours
▪ Narrow slots and precision cuts
▪ Tooling and fixture components
▪ Precision features in conductive metal parts
Need precision wire EDM parts for your project? Send us your drawings for an engineering review and quote.
Precision Inspection for EDM & Wire EDM Parts
We inspect critical dimensions, profiles, and narrow features to ensure EDM components meet specified drawing requirements.
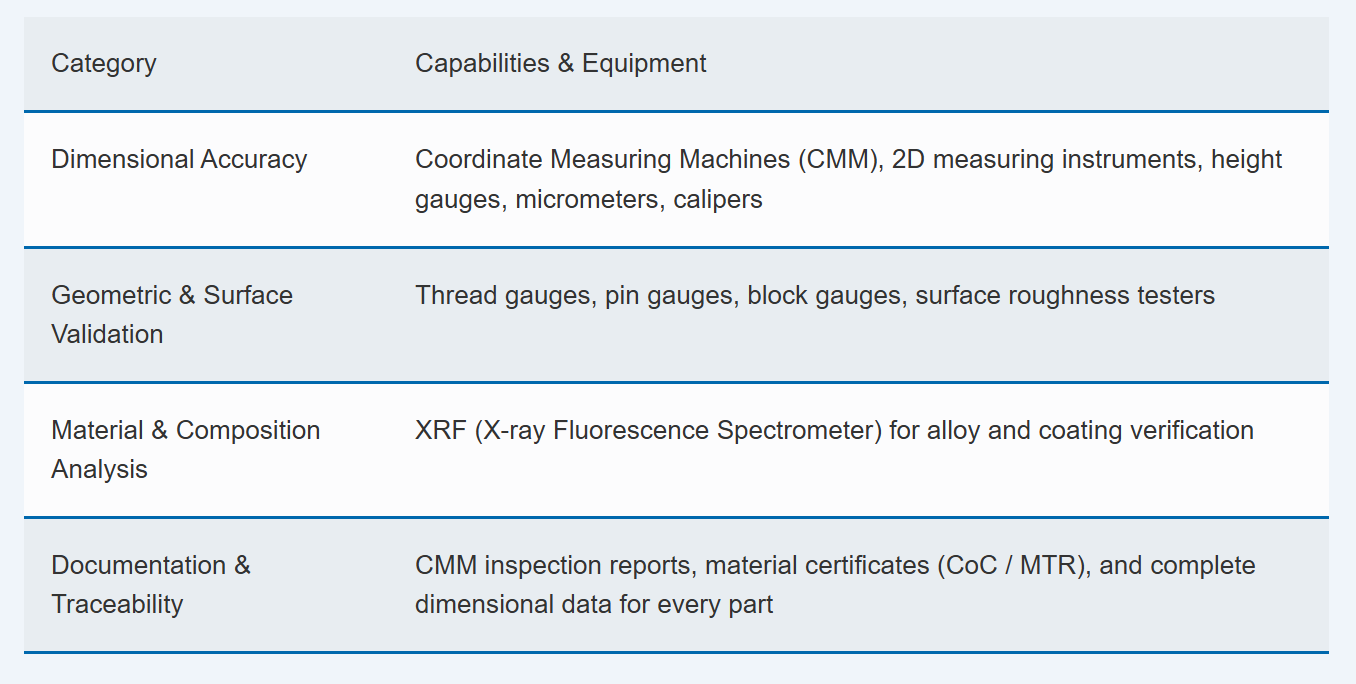
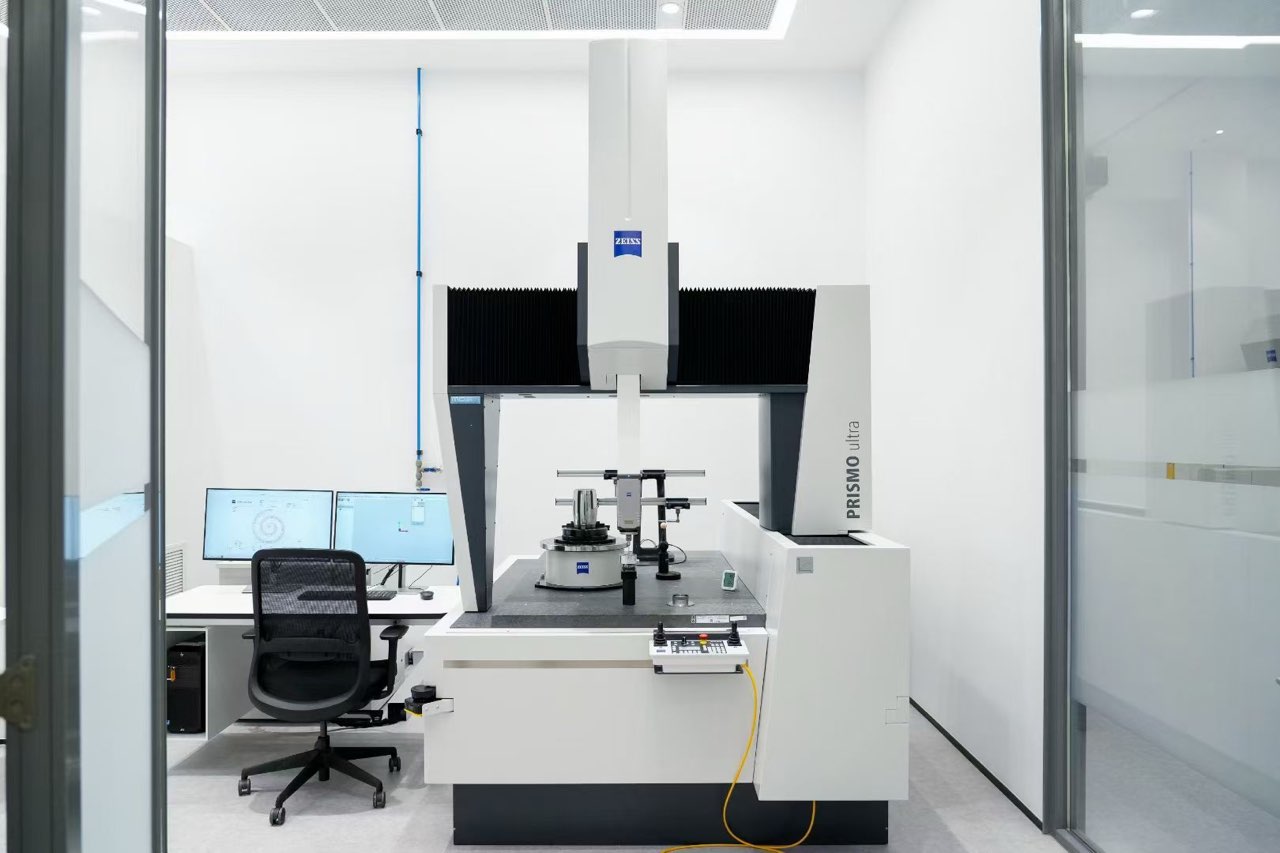
▪ Profile and dimensional inspection
▪ Slot and feature measurement
▪ Drawing compliance verification
Why Choose SelenPreci for EDM & Wire EDM
EDM and Wire EDM Services FAQ
Sinker EDM fits deep cavities, intricate profiles and tiny internal features on hard metals. Wire EDM excels at narrow kerf cutting and precise internal contours. Send us your CAD files and specifications, our engineers will recommend the proper process.
We process all conductive materials such as tool steel, stainless steel, Inconel, titanium, tungsten and carbide. Wire EDM requires conductive raw material. Contact us to confirm feasibility for special alloys.
Standard lead time is 3–10 working days, determined by part complexity, quantity and post-processing. Expedited service is available for urgent prototype and small-batch orders.
Wire EDM can reach ±0.005 mm normally, and ±0.002 mm for critical features. Sinker EDM maintains ±0.01 mm. We adopt CMM and toolmaker’s microscope for inspection, dimensional reports are available upon request.
Submit 2D drawings and 3D CAD files (STEP, IGES, DXF) through our quote form. Complete information including material, quantity, finish and tolerance helps speed up quotation. Our engineers reply within 24 hours.